Simple Distillation Unit

  • Home
  • Simple Distillation Unit

Simple Distillation Unit

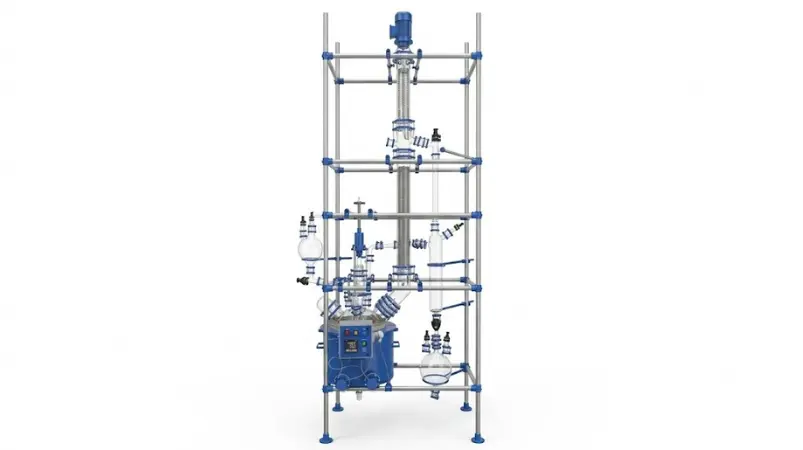
The Simple Distillation Unit is a high-efficiency industrial glass distillation system designed for basic vapor–liquid separation processes in chemical, pharmaceutical, and process industries. Manufactured using high-quality Borosilicate Glass 3.3, this unit ensures thermal stability, chemical resistance, and long operational life.

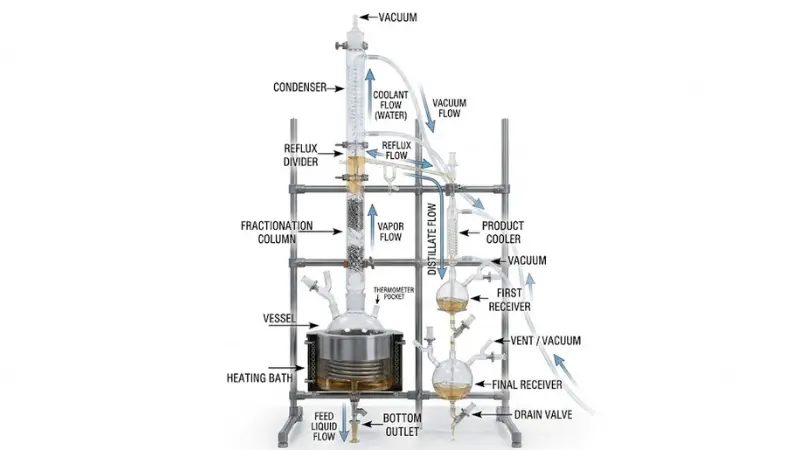
Our industrial simple distillation unit integrates a reaction vessel, heating bath, vertical condenser, and condensate receiver, enabling efficient separation of liquids based on boiling point differences. The system supports atmospheric as well as full vacuum operation, making it ideal for temperature-sensitive and volatile materials.

Available in 20 L to 500 L capacities, this modular simple distillation plant is suitable for pilot scale, R&D, and small-to-medium production operations.

How Does a Simple Distillation Unit Work? | Step-by-Step Process

  1. Charging the Feed Material
    The liquid mixture is charged into the borosilicate glass distillation vessel, which is securely mounted inside a temperature-controlled heating bath.

  2. Controlled Heating
    The heating bath gradually raises the temperature to the boiling point of the desired component, ensuring uniform heat transfer.

  3. Vapor Generation
    As heating continues, the lower boiling component vaporizes, while heavier components remain in the vessel.

  4. Vapor Condensation
    The vapor pass through a high-surface-area glass condenser, where cooling water converts vapor back into liquid.

  5. Condensate Collection
    The condensed liquid is collected in a receiver vessel with a drain valve, allowing safe and controlled discharge.

  6. Vacuum Operation (Optional)
    Under vacuum conditions, boiling occurs at lower temperatures, protecting heat-sensitive chemicals and improving efficiency.

Key Features & Benefits of Our Simple Distillation Unit

  • Borosilicate Glass 3.3 Construction – Superior chemical & thermal resistance
  • Atmospheric & Full Vacuum Compatible – Flexible operation
  • Modular & Expandable Design – Easy upgrades and scalability
  • Efficient Vertical Condenser – High condensation efficiency
  • Wide Capacity Range (20L–500L) – From lab to pilot production
  • Easy Cleaning & Maintenance – Smooth glass surfaces
  • Leak-Proof Joints & Precision Fabrication
  • Ideal for Continuous or Batch Distillation


Technical Specifications – Simple Distillation Unit

Model

Capacity

Heating Power (kW)

Condenser Line Size (DN)

Condenser Length (m)

SDU20

20 L

4.0

80 DN

0.35

SDU50

50 L

6.0

100 DN

0.50

SDU100

100 L

9.0

150 DN

1.50

SDU200

200 L

12.0

150 DN

1.50

SDU300

300 L

18.0

225 DN

2.50

SDU500

500 L

24.0

300 DN

4.00


Operating Conditions:

  • Pressure: Atmospheric to Full Vacuum

  • Material of Construction: Borosilicate Glass 3.3

  • Mounting: Heating bath with stable frame support


Industries We Serve with Simple Distillation Systems

  • Chemical Manufacturing Plants

  • Pharmaceutical & API Production

  • Solvent Recovery Units

  • Essential Oil & Aroma Chemical Industry

  • Petrochemical & Fine Chemical Processing

  • Research Laboratories & Pilot Plants

  • Educational & R&D Institutions

Applications of Simple Distillation Unit

  • Solvent purification & recovery

  • Separation of low-boiling liquids

  • Removal of volatile impurities

  • Chemical intermediate purification

  • Process development & pilot trials

  • Small-batch industrial distillation

Why Choose Our Simple Distillation Unit?

  • Manufacturer-Direct Pricing

  • Precision Flame-Worked Glass Fabrication

  • Custom Engineering Support

  • Global Export-Ready Design

  • Proven Performance in Industrial Environments

  • Trusted by Chemical & Pharma Industries

Our simple distillation units are designed not just as equipment—but as reliable process solutions that enhance yield, safety, and operational efficiency.

Customizable & Scalable Simple Distillation Systems

  • Custom vessel volumes

  • Alternative condenser designs

  • Vacuum system integration

  • Automation & instrumentation support

  • Integration with solvent recovery or scrubber systems

Contact us today to get a customized distillation solution for your industry!

Safety & Operating Advantages – Simple Distillation Unit

Our Simple Distillation Unit is designed with industrial-grade safety, process stability, and operator protection, making it ideal for chemical, pharmaceutical, and solvent recovery applications.

1) Explosion-Safe Borosilicate Glass 3.3 Construction
Ensures spark-free operation, excellent thermal shock resistance, and safe handling of flammable solvents.

2) Vacuum-Compatible Simple Distillation System
Supports atmospheric and full vacuum operation, enabling low-temperature distillation for heat-sensitive products.

3) No Metal Contamination
All product-contact parts are glass, ensuring high-purity distillate output required in API, pharma, and fine chemicals.

4) Uniform Heat Distribution via Heating Bath
Prevents localized overheating, reduces glass stress, and ensures consistent distillation performance.

5) Leak-Proof Joints & Precision Glass Fabrication
Minimizes vapour loss, improves process efficiency, and enhances operator safety.

6) Smooth Internal Glass Surfaces
Prevents residue buildup, allows easy cleaning, and supports GMP-friendly operations.

7) Vacuum Controller
For efficient low-pressure distillation and enhanced solvent recovery.

8) Chiller / Cooling Circulator System
Improves condenser efficiency and ensures stable condensation rates.

9) Digital Temperature Controller & Sensors
Enables precise temperature monitoring and control.

10) Additional Receiver Vessels with Drain Valve
Suitable for batch collection and fraction-wise separation.

11) Sight Glass & Sampling Port
Allows real-time process monitoring without disturbing the operation.

12) Integration with Solvent Recovery or Gas Scrubbing Systems
Ideal for emission control, environmental compliance, and solvent reuse.

13) All accessories are fully compatible with the base Simple Distillation System.

Frequently Asked Questions (FAQ) – Simple Distillation Unit

Q1. What is a Simple Distillation Unit used for?

A Simple Distillation Unit is used for separating and purifying liquids based on differences in boiling points. It is widely used in chemical processing, pharmaceutical manufacturing, solvent purification, and laboratory to pilot-scale operations.

Q2. Can the Simple Distillation Unit operate under vacuum?

Yes, our Industrial Simple Distillation Units are designed for both atmospheric pressure and full vacuum operation, allowing low-temperature distillation for heat-sensitive materials.

Q3. What material is used to manufacture the Simple Distillation Unit?

The unit is manufactured using high-quality Borosilicate Glass 3.3, offering excellent chemical resistance, thermal stability, and long service life.

Q4. What capacity options are available in Simple Distillation Units?

We offer Simple Distillation Units in 20 L, 50 L, 100 L, 200 L, 300 L, and 500 L capacities, suitable for laboratory, pilot, and industrial applications.

Q5. Is the Simple Distillation System suitable for continuous industrial use?

Yes, the system is engineered for reliable batch and semi-continuous operation in industrial environments, when operated within recommended parameters.

Q6. Can the Simple Distillation Unit be customized?

Absolutely. Our Simple Distillation Units are fully customizable, including capacity, condenser size, vacuum integration, automation, and accessory selection.

Related Products

Continuous Distillation System

View Details

Reaction Distillation Unit

View Details

Fractional Distillation Unit

View Details

Simple Distillation Unit

View Details