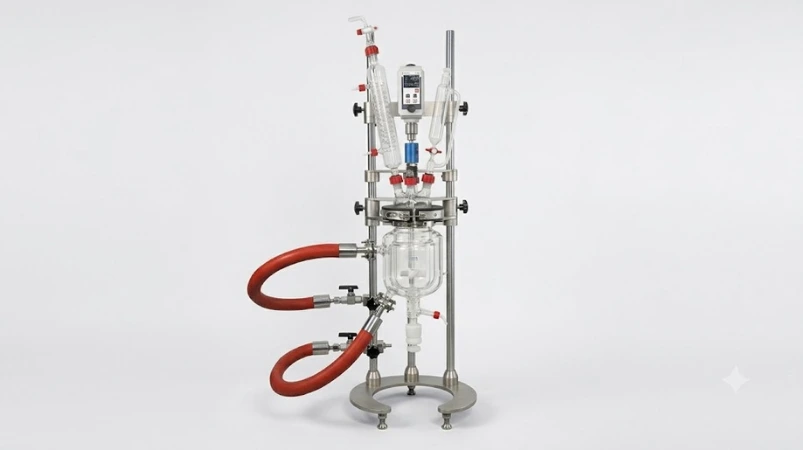
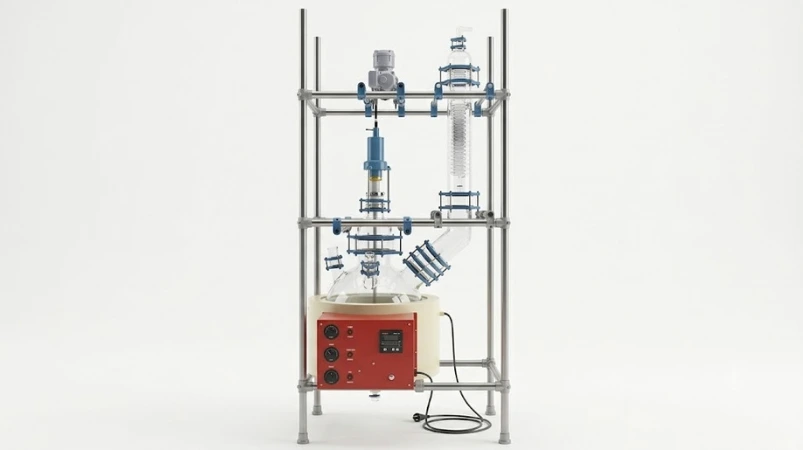
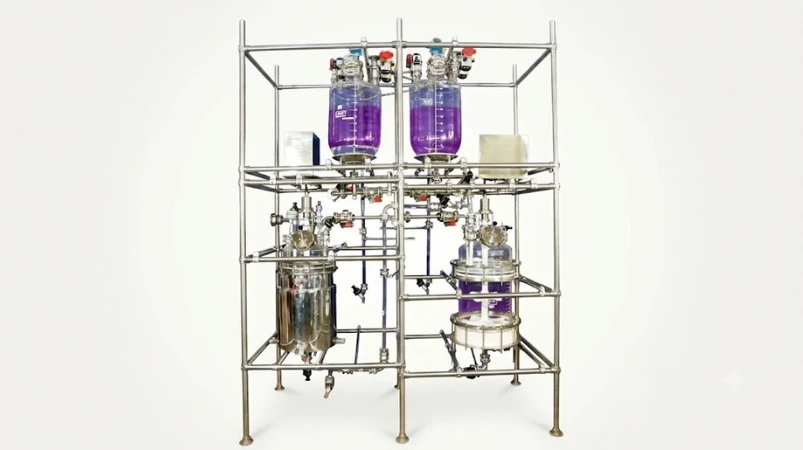
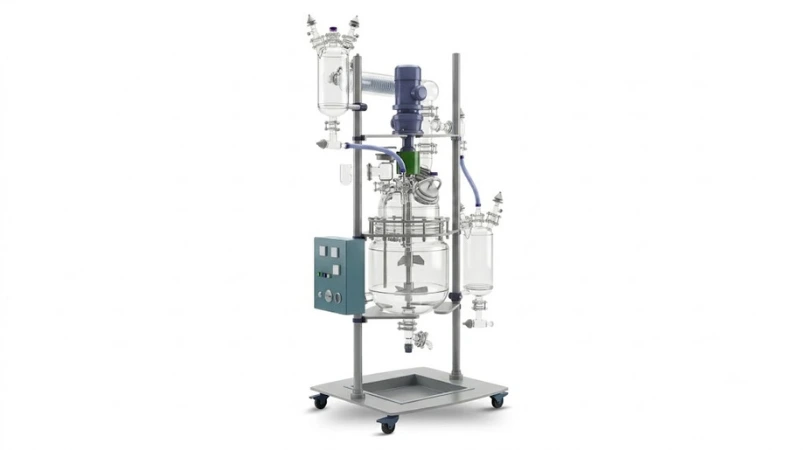
Our Kilo Lab Systems are advanced glass-based pilot and kilo-scale process platforms engineered to support process development, scale-up validation, and limited batch production under conditions that closely replicate full-scale industrial manufacturing.
Designed using premium Borosilicate Glass 3.3 (SCHOTT DURAN equivalent), these systems provide exceptional chemical resistance, thermal stability, and full process visibility, making them indispensable for pharmaceutical, fine chemical, and specialty chemical industries.
The Kilo Lab System acts as a critical bridge between laboratory R&D and commercial production, enabling safe, repeatable, and data-driven scale-up.
System Architecture & Design Philosophy
Kilo Lab Systems are not standalone reactors — they are fully integrated process assemblies engineered for reaction, distillation, filtration, and separation operations within a single scalable platform.
Core Design Highlights
Each system is custom-built based on process chemistry, batch size, operating conditions, and future scalability needs.
How Kilo Lab Systems Work (Process Flow)
This workflow allows precise replication of plant-level process behavior.
Integrated Sub-Systems Within Kilo Lab Systems
Our Kilo Lab Systems can incorporate the following core sub-products, matching or exceeding competitor offerings:
Advanced Glass Jacketed Reactor
Agitated Nutsche Filter (ANF)
Glass Lined Reactor Assembly
These systems can operate independently or as an integrated process line.
Key Features & Technical Strengths
Technical Specifications (Representative Range)
|
Parameter |
Specification |
|
Nominal Reactor Capacity |
20 L – 200 L |
|
Working Temperature |
–50°C to +180°C |
|
Design Temperature |
–60°C to +200°C |
|
Working Pressure |
Vacuum to +0.8 bar(g) |
|
Jacket Design Pressure |
–1 to +0.5 bar(g) |
|
Stirrer Speed |
20–192 RPM (Variable) |
|
Heat Transfer Area |
0.5 – 2.5 m² |
|
Vapour Line Size |
DN 50 – DN 100 |
|
Receiver Configuration |
Dual receivers for continuous operation |
|
Safety |
Rupture disc, vacuum relief, pressure control |
Safety, Control & EHS Compliance
Designed to meet strict Environmental, Health & Safety (EHS) standards.
Why Kilo Lab Systems Are Critical for Scale-Up
Kilo Labs enable fail-fast, learn-fast, and scale-safe development.
Industries We Serve
Optional Accessories & Customization
(Standardized accessory pool – mix & match)
Frequently Asked Questions (FAQs)
Q1. Is this suitable for API production?
Yes, ideal for small-batch API and intermediates.
Q2. Can it simulate full-scale production?
Yes, designed to replicate plant conditions accurately.
Q3. Can filtration and distillation be integrated?
Yes, ANF and distillation systems can be fully integrated.
Q4. Is customization available?
Completely customizable based on process requirements.
Why Choose Our Kilo Lab Systems?